Brightness Gain Is Not the Only KPI: How Mills Judge Deinking Trial Success
For a paper recycling mill, a deinking trial can look successful on the lab sheet and still fail on the floor. Brightness gain matters, but it is only one part of the operating picture. A trial that lifts brightness while increasing fiber loss, slowing drainage, pushing stickies forward, or destabilizing flotation is not a mill win.
Pulprift supports mills that evaluate enzyme-assisted deinking as a process change, not a single-number additive test. The right KPI set should show whether the enzyme program improves recovered fiber value while protecting throughput, cleanliness, and chemical discipline.
If you are comparing an enzyme supplier for paper deinking mills, the question is not only “How much brighter did the pulp get?” It is “Did the system run cleaner, drain faster, retain more usable fiber, and reduce pressure on caustic, peroxide, surfactant, or dispersant demand?”
Why brightness alone can mislead
Brightness is visible, easy to report, and commercially important. But brightness gain can be created in several ways, not all of them efficient.
A trial may show higher brightness because:
- ink detachment improved before flotation,
- flotation selectivity improved,
- chemical charge was pushed higher,
- fines or ash were removed aggressively,
- yield loss increased,
- washing load increased,
- stickies or dirt were dispersed rather than removed.
Only the first two are usually desirable by themselves. The rest may transfer cost elsewhere in the mill.
For recovered office waste, mixed office waste, newsprint grades, coated grades, or mixed furnish, Pulprift recommends judging enzyme deinking trials against a balanced KPI set: optical gain, fiber recovery, drainage, contaminant removal, wet-end stability, and operating cost.
The KPI stack for a serious deinking trial
1. Brightness gain at equivalent chemical conditions
Brightness should be measured against a stable baseline, not against a moving chemical target. If peroxide, caustic, silicate, chelant, surfactant, or collector strategy changes during the same window, the trial can become difficult to interpret.
A practical trial should ask:
- Did brightness increase at the same chemical charge?
- Can the same brightness be held with lower chemical demand?
- Was brightness stable across furnish variation?
- Did dirt count or residual ink move in the same direction?
Brightness gain is strongest when it comes with cleaner ink release and more selective removal, not simply harder chemistry.
2. Yield and usable fiber recovery
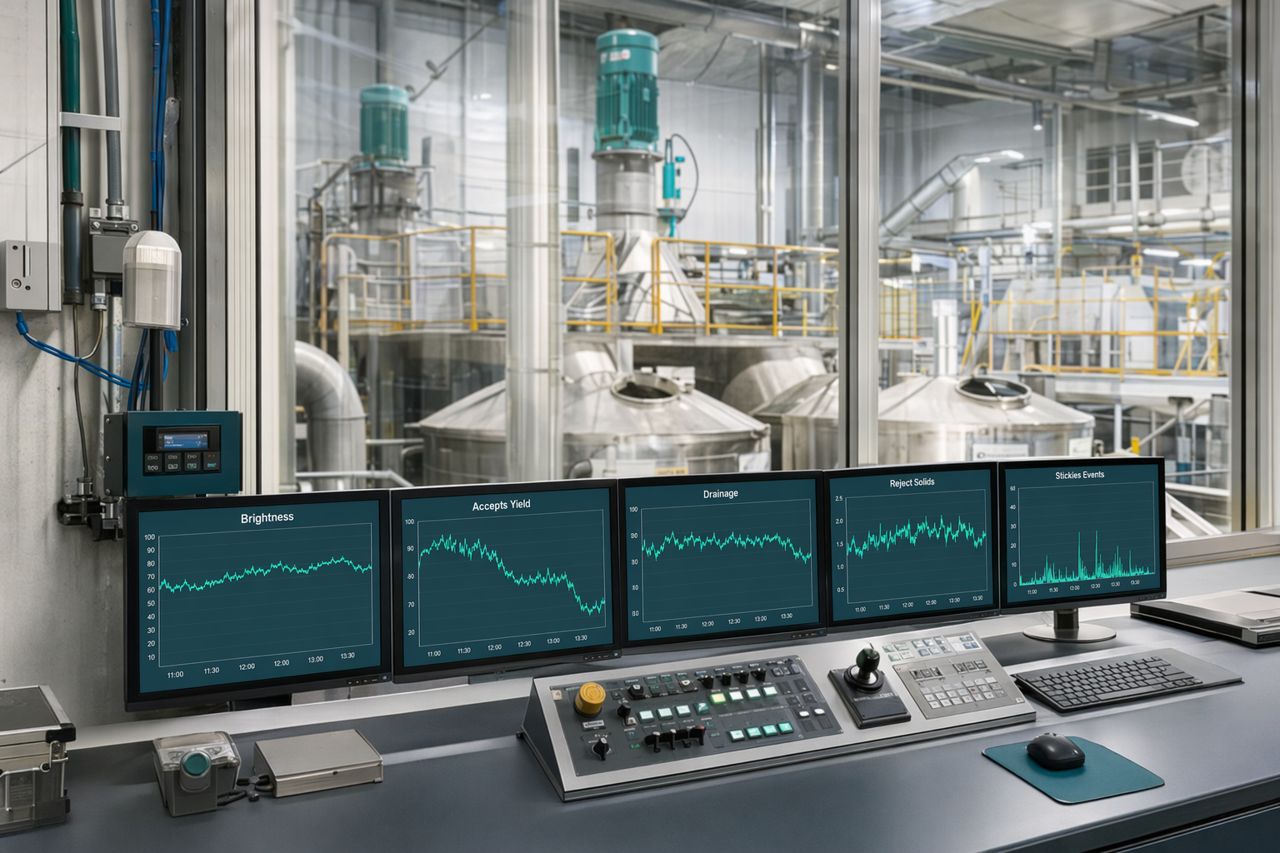
Yield is where many deinking trials are won or lost. A brightness increase that comes with higher rejects, excess fiber carryover in flotation froth, or stronger washing losses can reduce the value of the trial.
Track:
- accepts yield,
- flotation reject solids,
- fiber content in froth,
- screen reject movement,
- ash and fines balance,
- pulp strength indicators downstream.
The target is not maximum ink removal at any cost. The target is better optical cleanliness per unit of recovered fiber retained.
3. Drainage and thickening behavior
Enzyme-assisted deinking can affect how fibers, fines, inks, coatings, and stickies behave in water. Drainage is a critical operating KPI because it touches washer load, thickener stability, press section behavior, steam demand, and production rate.
Trial data should include:
- drainage response after pulping,
- washer or thickener throughput,
- filtrate clarity trend,
- white water solids behavior,
- press dewatering trend if the trial reaches the machine.
A useful enzyme program should support faster water release or at minimum maintain drainage while improving ink removal. If drainage slows, the mill needs to know whether the cause is furnish change, chemical interaction, fines liberation, or contaminant dispersion.
4. Stickies control and dirt movement
Recovered paper mills live with adhesive contamination. A deinking trial should not only detach ink; it must avoid creating a new stickies problem downstream.
Evaluate:
- macro stickies trend,
- micro stickies trend,
- deposits on screens, cleaners, flotation cells, washers, wires, felts, and rolls,
- pitch and adhesive tack behavior,
- dirt count and visible speck movement,
- wet-end deposit cleaning frequency.
A poor trial may break contaminants into smaller material that escapes early removal and shows up later as deposits, sheet defects, or downtime. A good trial improves ink release while keeping contaminant removal controlled and predictable.
5. Flotation selectivity
Flotation is not just about making foam. The foam must carry ink and unwanted contaminants without dragging out too much usable fiber.
Trial checks should include:
- froth stability,
- froth solids profile,
- ink load in reject stream,
- fiber loss in reject stream,
- air and surfactant sensitivity,
- cell cleanliness and overflow control.
Pulprift focuses on the interface between pulping chemistry, enzyme contact, ink detachment, and flotation response. The best result is not the biggest froth blanket. It is a froth stream that removes the right material.
6. Chemical reduction potential
Mills often investigate enzyme deinking to reduce pressure on caustic, peroxide, surfactant, dispersant, or other process aids. Chemical reduction should be tested after the baseline enzyme effect is understood.
A clean sequence is:
- Stabilize furnish and baseline operating conditions.
- Run the enzyme program at normal chemical charge.
- Confirm brightness, yield, drainage, and stickies response.
- Step down selected chemicals in controlled stages.
- Confirm that the optical and operating gains remain.
This prevents a promising enzyme trial from being rejected because too many variables moved at the same time.
Trial design: what mills should lock before judging results
A deinking trial needs enough discipline to separate enzyme effect from normal mill noise. Before the trial begins, align on:
- furnish type and expected variation,
- pulper consistency and temperature window,
- pulping time and shear profile,
- enzyme addition point,
- contact time before flotation or washing,
- pH window,
- flotation chemistry and air settings,
- screening and cleaning settings,
- sampling locations,
- baseline period and comparison period,
- acceptance criteria.
The most common trial failure is not poor enzyme performance. It is poor comparison structure. A mill cannot judge a biological process aid accurately if furnish, chemistry, pulping time, and reject handling are all shifting without documentation.
Recommended acceptance matrix
Use a simple pass/fail and weighted-score matrix. Brightness gets a score, but it should not dominate the decision.
| KPI area |
What to confirm |
Good trial signal |
| Brightness and dirt |
Optical gain and lower visible contamination |
Cleaner pulp without overdriving chemistry |
| Yield |
Accepts yield and fiber loss in rejects |
More saleable fiber retained |
| Drainage |
Washer, thickener, and machine dewatering trend |
Equal or faster water release |
| Stickies |
Macro and micro stickies behavior |
Lower deposits or no downstream penalty |
| Flotation |
Reject selectivity and froth behavior |
Ink-rich rejects with controlled fiber loss |
| Chemistry |
Reduction opportunity |
Same target quality with lower chemical pressure |
| Runnability |
Downtime, cleaning, sheet defects |
Fewer interruptions and cleaner equipment |
| Cost position |
Total process economics |
Better cost per accepted tonne of usable pulp |
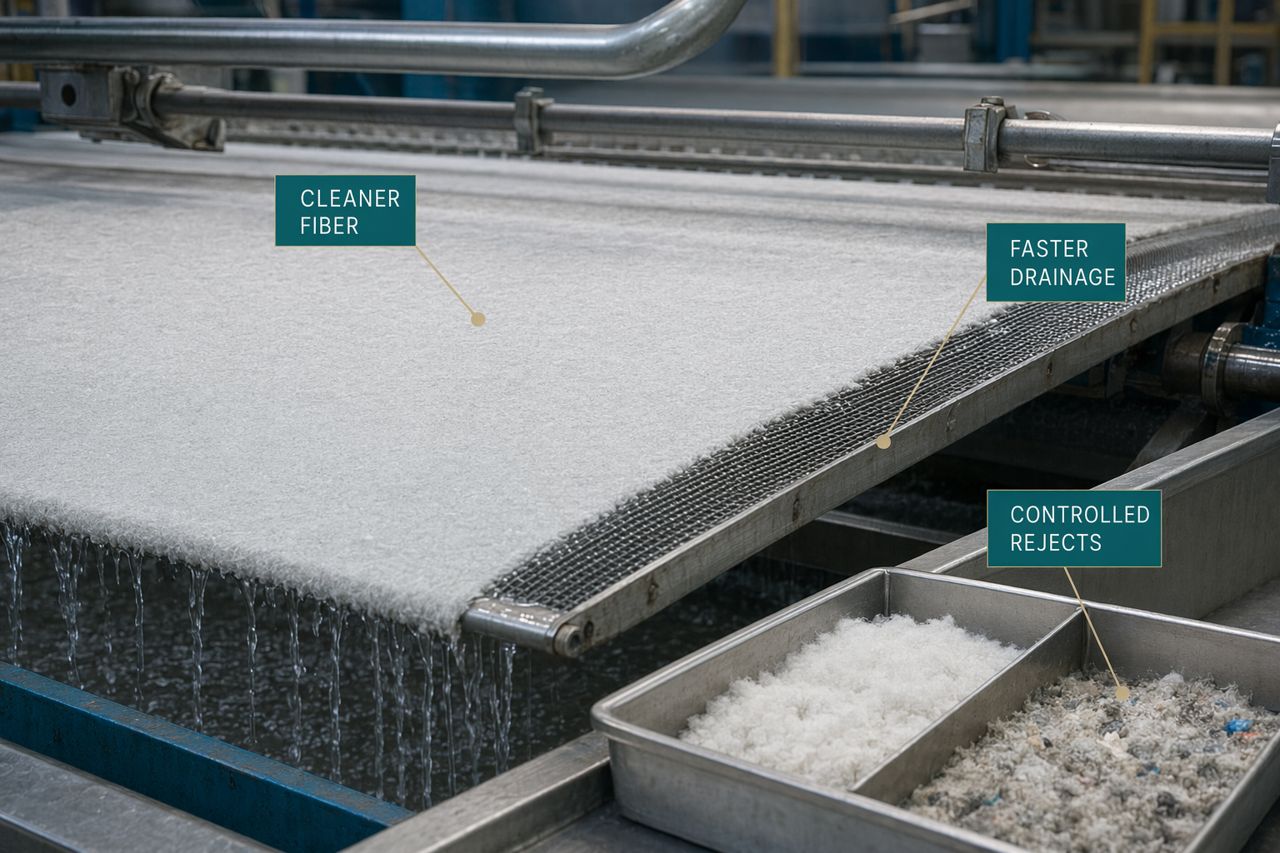
The strongest trials show improvement across several rows. A single brightness gain is useful. A balanced operating gain is bankable.
Where Pulprift fits in the mill evaluation
Pulprift enzyme solutions are built for paper recycling mills that want practical deinking improvements without losing sight of the whole line. We help mills define the trial window, select the addition point, protect drainage, and compare outcomes against production realities.
Typical objectives include:
- improving ink detachment during pulping,
- supporting brightness gain at stable chemistry,
- improving flotation selectivity,
- reducing fiber loss in rejects,
- maintaining or improving drainage,
- reducing chemical pressure where the process allows,
- lowering deposit-related downtime risk.
We do not treat deinking as a lab-only brightness exercise. The value is proven when the pulp is cleaner, the system is stable, and the mill can keep running.
Practical trial questions to ask before requesting supply
Before starting a deinking enzyme trial, your team should answer:
- Which furnish is the trial meant to improve?
- Is the commercial target higher brightness, lower chemical cost, higher yield, better drainage, fewer stickies, or a combination?
- Where is the best addition point for enzyme contact?
- Which variables must stay fixed during the comparison?
- What reject, filtrate, and accepts samples will be collected?
- What downtime or cleaning events will be logged?
- What result would justify scale-up?
These answers make supplier comparison easier and keep the trial connected to mill economics.
Request a quote for a deinking enzyme trial
If your mill is planning a deinking trial, Pulprift can help structure the enzyme selection around your furnish, pulper conditions, flotation setup, drainage limits, and quality target.
Use the on-site request a quote form to share your furnish type, target grade, current deinking pain points, and preferred trial window. We will respond with a practical supply recommendation and trial support plan.