How Paper Mills Document Production Trials Without Confusing Shift Noise for Real Gains
Production trials in a paper recycling mill can look better than they are — or worse than they are — if the mill team does not separate process noise from real movement.
Recovered fiber systems are naturally variable. Furnish changes by load. Ash moves. Ink chemistry shifts. Stickies load can swing across a single day. Operators adjust dilution, chemistry, rejects, air, temperature, and consistency to keep the line stable. If a trial is judged from one good shift, one lab sheet, or one cleaner run, the conclusion is usually weak.
For mills evaluating an enzyme supplier for paper deinking mills, the documentation has to be tight enough to answer one question clearly:
Did the enzyme program create a repeatable process gain under normal mill conditions, or did the mill simply catch a favorable operating window?
Pulprift recommends documenting production trials around baseline control, matched operating windows, agreed KPIs, and shift-level discipline. The goal is not to create paperwork. The goal is to make the trial defensible when production, technical, purchasing, and mill management review the same data.
Why production trial documentation fails
Most unclear enzyme trials fail for one of five reasons:
-
The baseline is too short
One or two shifts rarely capture normal furnish and operating variation.
-
The trial window is not matched to the baseline
Comparing a clean weekday furnish to a heavy weekend furnish makes the data hard to use.
-
Operators change too many variables at once
If caustic, peroxide, surfactant, dispersant, pulper temperature, retention, flotation air, and enzyme dosage all move together, the mill cannot assign the result.
-
Only final sheet brightness is reviewed
Brightness matters, but it is not the only mill outcome. Drainage, ash carryover, rejects, foam behavior, stickies, and runnability may tell the stronger story.
-
Shift comments are missing
A lab number without operating context is easy to misread. Screen plugging, broke return, furnish changes, chest level swings, and downtime events must be captured.
A good production trial does not remove all variability. It makes variability visible.
Start with a written trial objective
Before enzyme is introduced, write the trial objective in mill language.
Examples:
- Increase deinked pulp brightness while holding yield within the current operating range.
- Reduce stickies-related deposits in screening, cleaning, or paper machine approach flow.
- Improve drainage and washing efficiency without increasing fiber loss.
- Reduce selected deinking chemicals while maintaining brightness and dirt performance.
- Stabilize flotation response across variable recovered office paper or mixed recovered furnish.
Avoid vague goals such as “improve deinking.” A production trial needs a primary objective and a short list of secondary observations.
Define the primary KPI
Choose one primary KPI before the trial starts. Common choices include:
- Brightness gain after deinking
- Residual ink reduction
- Stickies count or deposit tendency
- Drainage improvement
- Yield protection at comparable rejects
- Chemical reduction at comparable pulp quality
- Downtime or cleaning frequency related to deposits
Secondary KPIs can be tracked, but the trial should not be declared successful by moving the target after the data comes in.
Build a baseline that reflects normal operation
A baseline is not just a set of lab results. It is a record of how the mill normally runs before the enzyme program is added.
A practical baseline should capture:
- Furnish type and supplier mix
- Pulper consistency and retention window
- pH and temperature range in the application zone
- Existing deinking chemistry program
- Flotation or washing operating conditions
- Screen and cleaner rejects
- Thickener or washer performance
- Brightness and dirt trend
- Stickies observations
- Drainage behavior
- Downtime, cleanouts, and plugging events
- Operator comments by shift
For many mills, a useful baseline covers several production days under representative furnish. If the furnish changes materially, mark it clearly. Do not average unlike conditions and call it control.
Match the enzyme trial window to the baseline
The cleanest trial compares similar operating windows.
Try to match:
- Furnish grade and supplier pattern
- Production rate
- Pulping temperature
- Pulper retention
- pH range
- Consistency
- Existing chemical set points
- Flotation air and level control
- Washing and thickening conditions
- Paper machine grade target, if applicable
The enzyme does not need perfect laboratory conditions to show value. It does need a fair comparison.
If the mill must change a major variable during the trial, document it immediately. A clearly marked upset does not ruin a trial. An unmarked upset can ruin the interpretation.
Control the number of moving parts
The most common documentation problem is running an enzyme trial and a chemical optimization trial at the same time.
That can be done later. First, establish whether the enzyme program creates a measurable process response under current conditions.
A disciplined sequence often works better:
- Baseline under current chemistry
- Enzyme introduction with current chemistry held steady
- Stabilization period after dosage reaches the process
- KPI tracking across matched shifts
- Optional chemical reduction step after response is confirmed
This structure helps the mill avoid crediting the enzyme for a caustic change, peroxide correction, surfactant move, furnish improvement, or operator adjustment.
Record the application window, not just the dosage
For enzyme deinking trials, the application window matters.
Document:
- Addition point
- Contact time before flotation, washing, or screening
- Temperature range
- pH range
- Consistency
- Mixing condition
- Sequence relative to caustic, peroxide, surfactant, dispersant, and bleaching chemistry
- Time required for treated pulp to reach the sampling point
This is especially important in recovered fiber systems with large chests and long residence times. A sample pulled too early may represent untreated or partially treated stock. A sample pulled after a furnish change may represent the wrong comparison.
Mark the process delay on the trial sheet so each lab result is tied to the correct treatment window.
Use shift-level trial sheets
A production trial should be easy for operators to document without slowing the floor.
A good shift sheet captures:
- Date and shift
- Furnish description
- Production rate
- Enzyme on/off status
- Addition point and pump status
- Key chemistry set points
- Pulper pH and temperature range
- Flotation or washing status
- Brightness and dirt results
- Stickies or deposit observations
- Drainage or freeness trend where used by the mill
- Rejects trend
- Downtime and plugging events
- Operator notes
Operator notes are often the difference between useful and misleading data. A brightness drop may be explained by a furnish load. A drainage gain may align with better washing. A stickies event may trace to broke return or a supplier change.
Numbers need context.
Do not over-average the data
Averages are useful, but they can hide the trial story.
Review the data in layers:
1. Time trend
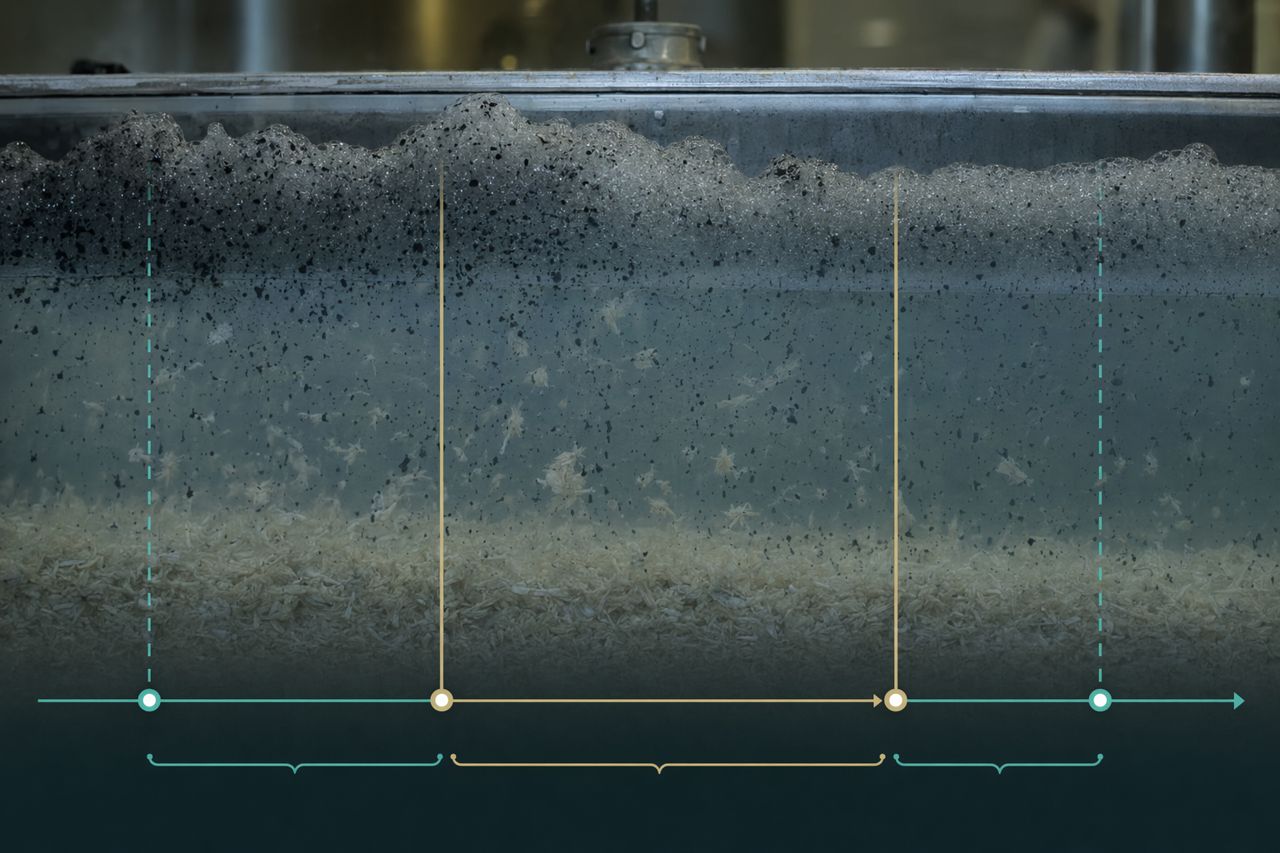
Plot baseline and trial data by time. Look for when treated stock should have reached the measurement point.
2. Matched operating windows
Compare shifts with similar furnish, rate, pH, temperature, and chemistry.
3. Upset-excluded view
Separate known upsets such as screen plugging, furnish interruption, chemical outage, major grade change, or abnormal broke return.
4. Full-period view
Keep the full-period average visible, but do not let it override the operating reality.
The strongest trial conclusion is usually not “the average moved.” It is “the same process window repeatedly ran better with the enzyme program in place.”
Track brightness without ignoring mill economics
Brightness gain is often the headline KPI in deinking trials, but the mill should document the economic levers behind it.
Relevant questions include:
- Did brightness improve at the same chemical cost?
- Could the mill hold brightness while reducing selected chemicals?
- Did residual ink or dirt trend improve with the same furnish?
- Did flotation reject load change?
- Did fiber yield stay stable?
- Did drainage improve enough to support throughput or lower steam demand downstream?
- Did deposit-related downtime or wash-up frequency change?
A trial that improves brightness but increases fiber loss may not be attractive. A trial that holds brightness while reducing chemical pressure and improving runnability may be more valuable.
Document both pulp quality and operating cost direction.
Include stickies and deposit behavior
Stickies control is difficult to summarize in one number, but it should not be left out.
Track practical mill indicators:
- Screen basket fouling
- Cleaner plugging
- Felt, wire, or roll deposits
- Sheet defects associated with tacky contaminants
- White water contamination trend
- Cleaning frequency
- Unplanned downtime tied to deposits
- Operator observations at known problem points
If the mill has a standard internal method for stickies or deposit tendency, use it consistently across baseline and trial. The key is not the method name. The key is repeatability under comparable process conditions.
Document chemical reduction as a second step
Many mills evaluate enzymes to reduce chemical load. That is valid, but the reduction should be staged.
A practical approach:
- Confirm enzyme response with existing chemistry held steady.
- Identify which chemical lever is the reduction target.
- Reduce one lever at a time.
- Hold the new setting long enough to see treated stock through the system.
- Compare brightness, dirt, stickies, drainage, yield, and runnability against baseline.
Do not reduce multiple chemicals at once unless the trial objective is broad system reformulation and the mill accepts a less precise attribution.
For purchasing and management review, the most credible case is a controlled sequence showing quality maintained or improved while chemical demand moves down.
Align sampling with process residence time
Recovered fiber systems have delays. Pulper changes do not appear instantly at flotation accepts, washers, storage chests, or the paper machine.
Before the trial, estimate the residence time from enzyme addition to each sampling point.
Mark:
- Enzyme start time
- Expected arrival at primary sample point
- Expected arrival at secondary sample points
- Any chest level swings that may dilute or delay the response
- Any bypasses, recirculation loops, or broke additions
This prevents the team from sampling the wrong stock and calling it enzyme performance.
Separate production noise from real gain
A real gain usually has three traits:
-
Timing
The improvement appears after treated stock reaches the measurement point.
-
Repeatability
The improvement appears across more than one comparable shift or furnish window.
-
Process fit
The direction of movement makes operational sense. For example, better ink release should align with improved flotation response, dirt reduction, or brightness movement under matched chemistry.
A suspicious gain often has one of these traits:
- It appears before treated stock could reach the sample point.
- It occurs during a major furnish improvement.
- It disappears when the furnish returns to normal.
- It depends on several simultaneous chemistry changes.
- It is visible in one lab result but not in the process trend.
The point is not to reject good news. The point is to make sure the mill can trust it.
What a clean trial summary should include
At the end of the trial, the summary should be short enough for management and detailed enough for technical review.
Include:
- Trial objective
- Baseline period and conditions
- Enzyme application point and operating window
- Trial period and matched conditions
- Primary KPI result
- Secondary KPI observations
- Chemical settings before and during the trial
- Furnish notes
- Upsets excluded or marked
- Operator observations
- Production impact
- Estimated economic direction
- Recommendation for next step
The best summaries do not oversell. They show what moved, under what conditions, and what the mill should test next.
When to extend the trial
Extend the trial if:
- Furnish changed too much to compare fairly.
- The enzyme was not in the correct application window long enough.
- A pump, feed line, or dilution issue affected delivery.
- A major process upset occurred during most of the trial period.
- The KPI moved in the right direction but needs repeat confirmation.
- Chemical reduction was attempted before enzyme response was established.
Stopping too early can reject a useful program. Running too long without discipline can create a data pile that still does not answer the question.
A trial extension should have a specific reason and a specific decision point.
Pulprift’s view on trial discipline
Pulprift supports paper recycling mills with enzyme programs designed for deinking, fiber recovery, drainage improvement, and deposit pressure reduction. But product fit is only part of a successful trial.
A well-documented production trial protects the mill from false positives and false negatives. It helps pulping managers explain results to quality, operations, maintenance, purchasing, and leadership without relying on selective anecdotes.
For mills comparing enzyme options, the stronger supplier is not only the one with a promising formulation. It is the one that helps the mill define the operating window, protect the baseline, read the process delay, and document the result in a way the site can act on.
Request a quote for a documented mill trial
If your mill is planning a deinking, stickies control, drainage, or chemical reduction trial, Pulprift can help define the application window and supply an enzyme program matched to your recovered fiber system.
Request a quote through the on-site contact form and include your furnish type, deinking layout, target KPI, and preferred trial window. We will respond with a practical supply recommendation and the process details needed to run a clean evaluation.